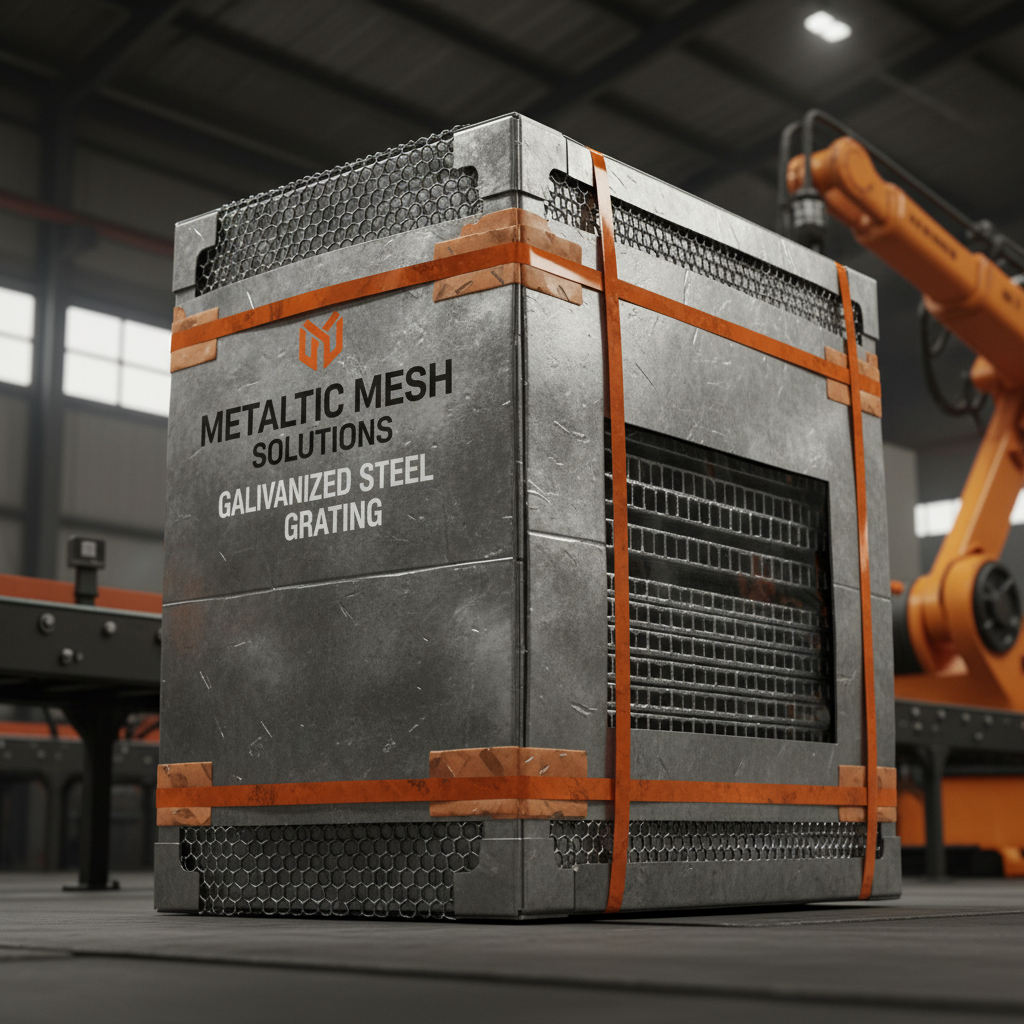
In the demanding world of industrial infrastructure and heavy-duty construction, the need for stable, high-load bearing surfaces is paramount. Whether dealing with bridge decking or industrial flooring, the integration of robust materials often requires specialized solutions to ensure longevity and safety. This is where the concept of enhancing structural stability through a concrete weight coating approach becomes essential for engineers seeking to optimize load distribution.
Global infrastructure projects are increasingly facing the challenge of extreme environmental wear, where traditional steel grating alone may not suffice against repetitive heavy impact. The industry is shifting toward integrated systems that combine the high strength of riveted gratings with advanced protective measures. Understanding the synergy between structural steel and a concrete weight coating methodology allows for the creation of platforms that resist fatigue and chemical erosion more effectively.
By examining the technical specifications of riveted gratings—manufactured through cold-press riveting of straight bearing bars to crimped rectangular flat bars—we can see how these products provide a foundation for high-capacity loads. When paired with the strategic logic of a concrete weight coating, these gratings transform into indestructible surfaces suitable for the harshest industrial zones, from alkali-rich environments to heavy-traffic bridge decks.
The Industrial Significance of Concrete Weight Coating
The global drive toward sustainable and resilient infrastructure has placed a renewed focus on how we protect and reinforce load-bearing surfaces. In sectors like bridge construction and heavy industrial plant management, the application of a concrete weight coating logic is vital for mitigating the risks of structural fatigue. By utilizing riveted gratings—which are cold-pressed for superior resistance—industries can create surfaces that handle repetitive loads without compromising integrity.
Beyond simple strength, the industrial significance lies in the ability to resist harsh chemical environments. Riveted gratings made from stainless steel or aluminum, when integrated with a concrete weight coating mindset, provide outstanding alkali and acid resistance. This ensures that walkways, trench covers, and drainage systems maintain their functionality even when exposed to corrosive industrial runoff or saltwater spray.
Defining the Mechanics of Concrete Weight Coating
At its core, a concrete weight coating refers to the strategic application of dense, protective layers or the integration of heavy-duty materials to increase the ballast and stability of a surface. In the context of steel gratings, this involves leveraging the high load capacity of riveted bars to support overlying weights, ensuring that the surface does not shift or vibrate under extreme pressure.
This process is deeply connected to modern humanitarian and industrial needs, where rapid deployment of stable flooring is required in disaster-prone areas or remote mining zones. The synergy between a high-strength riveted grating—available in carbon, stainless, or aluminum steel—and a concrete weight coating creates a composite effect that maximizes the lifespan of the installation.
Technically, this means the bearing bars and cross bars are spaced precisely (such as the RG12 and RG18 specifications) to provide a rigid grid. This grid acts as the skeletal support for any subsequent coating, ensuring that the concrete weight coating adheres firmly and distributes weight evenly across the entire structure, preventing localized failure points.
Core Components for Maximum Durability
The first pillar of durability is Material Selection. Depending on the environment, choosing between carbon steel for raw strength, stainless steel for corrosion resistance, or aluminum for lightweight agility is crucial. When implementing a concrete weight coating, the material of the underlying grating determines how well the coating bonds and how the overall system reacts to thermal expansion.
The second pillar is Surface Treatment. Whether the grating is galvanized, painted, or mill finished, the surface type—plain or serrated—plays a huge role. A serrated surface, in particular, provides an anti-slip grip and a mechanical lock for any concrete weight coating, ensuring that the protective layer remains intact even under the friction of heavy machinery.
Finally, Structural Geometry, defined by the bearing bar spacing and cross bar dimensions, ensures scalability. For instance, the RG18 series with its 1-1/8" spacing provides a different load-bearing profile than the RG12 series. This geometric precision is what allows a concrete weight coating to remain stable across large spans, such as bridge decking or industrial platforms.
Global Applications and Use Cases
Across the globe, the application of reinforced surfaces utilizing a concrete weight coating logic is seen in critical infrastructure. In North American and European bridge constructions, riveted steel gratings are used as heavy-duty bridge decking to provide traffic surfaces that are both lightweight and incredibly strong. The addition of weight-stabilizing coatings helps in reducing wind-induced vibration and increasing the overall damping of the structure.
In the Asia-Pacific region, particularly in industrial zones and chemical plants, these systems are utilized as trench covers and drainage covers. Because the riveted grating is resistant to acids and alkalis, the concrete weight coating ensures that these covers remain in place despite the high-pressure flow of liquids beneath them, providing a safe, non-slip walkway for personnel.
Performance Comparison of Concrete Weight Coating Methods
Long-Term Value and Sustainability
Investing in high-quality riveted gratings paired with a concrete weight coating provides immense long-term financial value. By extending the lifespan of the flooring through corrosion resistance and impact durability, companies significantly reduce their maintenance cycles. This reliability fosters a sense of trust and safety for workers operating in hazardous environments, where a failure in the flooring could lead to catastrophic accidents.
From a sustainability perspective, these materials are highly eco-friendly. Steel and aluminum are 100% recyclable, meaning that at the end of a structure's lifecycle, the components can be reclaimed. The use of a concrete weight coating often reduces the need for frequent replacements, thereby lowering the overall carbon footprint associated with the production and transport of new industrial steel.
Future Trends in Structural Coatings
The future of structural reinforcement is moving toward "smart" coatings. We are seeing the emergence of sensors embedded within the concrete weight coating that can detect stress fractures or corrosion in the underlying riveted grating in real-time. This digital transformation allows for predictive maintenance, where repairs are made before a failure occurs.
Furthermore, the integration of green energy materials, such as carbon-sequestering concrete, is becoming a priority. These new types of concrete weight coating not only provide the necessary ballast and protection for steel gratings but also actively reduce the amount of CO2 in the atmosphere, aligning industrial growth with global climate goals.
Automation in the application process is also accelerating. Robotic spraying and precision riveting are ensuring that the tolerances between the grating and the concrete weight coating are tighter than ever, leading to more uniform load distribution and an even longer operational lifespan for bridge decking and platforms.
Overcoming Implementation Challenges
One of the primary challenges in implementing a concrete weight coating is ensuring the perfect bond between the organic coating and the inorganic steel. If the surface is not properly treated—whether through galvanization or a specific mill finish—the coating may peel under extreme thermal fluctuations. Expert insight suggests using serrated surfaces to create a mechanical bond that resists delamination.
Another hurdle is the weight trade-off. While increasing the weight of the coating improves stability, it can add unnecessary stress to the supporting structure. To solve this, engineers are now utilizing aluminum riveted gratings, which offer a lightweight foundation that offsets the added mass of the concrete weight coating, maintaining a high strength-to-weight ratio.
Finally, cost can be a barrier for smaller projects. However, by analyzing the total cost of ownership (TCO), it becomes clear that the initial investment in a high-grade concrete weight coating system is far lower than the cost of frequent repairs and downtime. Strategic planning and the use of standardized RG specifications help in controlling costs while maintaining high quality.
Analysis of Structural Performance and Coating Efficiency
| Grating Type |
Coating Compatibility |
Load Capacity |
Lifespan Score |
| Carbon Steel RG18 |
High (Galvanized) |
Excellent |
8/10 |
| Stainless Steel RG12 |
Very High (Mill) |
High |
10/10 |
| Aluminum Riveted |
Moderate (Painted) |
Medium |
7/10 |
| Serrated Carbon Steel |
Extreme (Mechanical) |
Excellent |
9/10 |
| Galvanized RG18 |
High (Chemical) |
Excellent |
8/10 |
| Custom Riveted Mesh |
Variable |
Variable |
7/10 |
FAQS
The primary purpose is to increase structural stability, provide a protective ballast layer, and enhance the load-bearing capacity of the underlying grating. By adding a dense coating, the system can better resist repetitive heavy impacts and vibrations, which is critical for bridge decking and heavy-duty industrial platforms.
Riveted gratings are cold-pressed, providing superior resistance to fatigue and impact compared to welded alternatives. Their rigid structure and available serrated surfaces provide a high-strength foundation and a mechanical lock, ensuring the concrete weight coating adheres firmly without slipping or cracking under pressure.
Stainless steel is the gold standard for corrosive environments due to its inherent alkali and acid resistance. However, galvanized carbon steel is also a highly effective and cost-efficient choice. When these are paired with a specialized weight coating, they create an impenetrable barrier against rust and chemical erosion.
Yes, aluminum riveted gratings are an excellent choice when weight reduction is necessary. While aluminum has a lower density than steel, its high strength-to-weight ratio allows it to support the coating while reducing the overall dead load on the supporting bridge or platform structure.
The choice depends on your load requirements and the thickness of your intended coating. RG18 generally offers a different bearing bar spacing and strength profile than RG12. Consult the technical data sheets to match the spacing (e.g., 1-1/8" for RG18) with the weight and thickness of the coating to ensure optimal load distribution.
Yes, because both the steel/aluminum gratings and many modern coating materials are 100% recyclable. Additionally, by significantly extending the lifespan of the infrastructure and reducing the frequency of replacements, these systems lower the total consumption of raw materials and energy over time.
Conclusion
In summary, the integration of high-strength riveted gratings with a strategic concrete weight coating provides an unparalleled solution for industrial flooring and bridge decking. By combining the mechanical resilience of cold-pressed steel—available in various materials and specifications like RG12 and RG18—with the stability of protective coatings, industries can achieve a perfect balance of durability, safety, and chemical resistance.
As we move toward a future of smarter, greener infrastructure, the adoption of these reinforced systems will be key to reducing maintenance costs and environmental impact. We recommend that engineers prioritize the synergy between surface treatment and coating selection to maximize the lifespan of their assets. For high-quality structural solutions, visit our website: www.cndowelltech.com.